
Quality control · 23 May 2026
From Finish Sample to Final Inspection
How finish approval, incoming-part checks, in-process inspection and final release can make a custom entrance more predictable.
Quality begins before assembly
Customisation adds choices, but it should not remove control. The project needs an approved configuration, physical finish sample and hardware schedule before production starts. Those references give purchasing, production and inspection the same definition of the product.
Four finish directions in the source range
EPIN TOMCIM's current China-market material groups its surface development into metallic fluorocarbon, liquid-metal effect, antique copper-look and fluorocarbon art-texture families. Each direction can produce a different response to light, touch and architectural context.
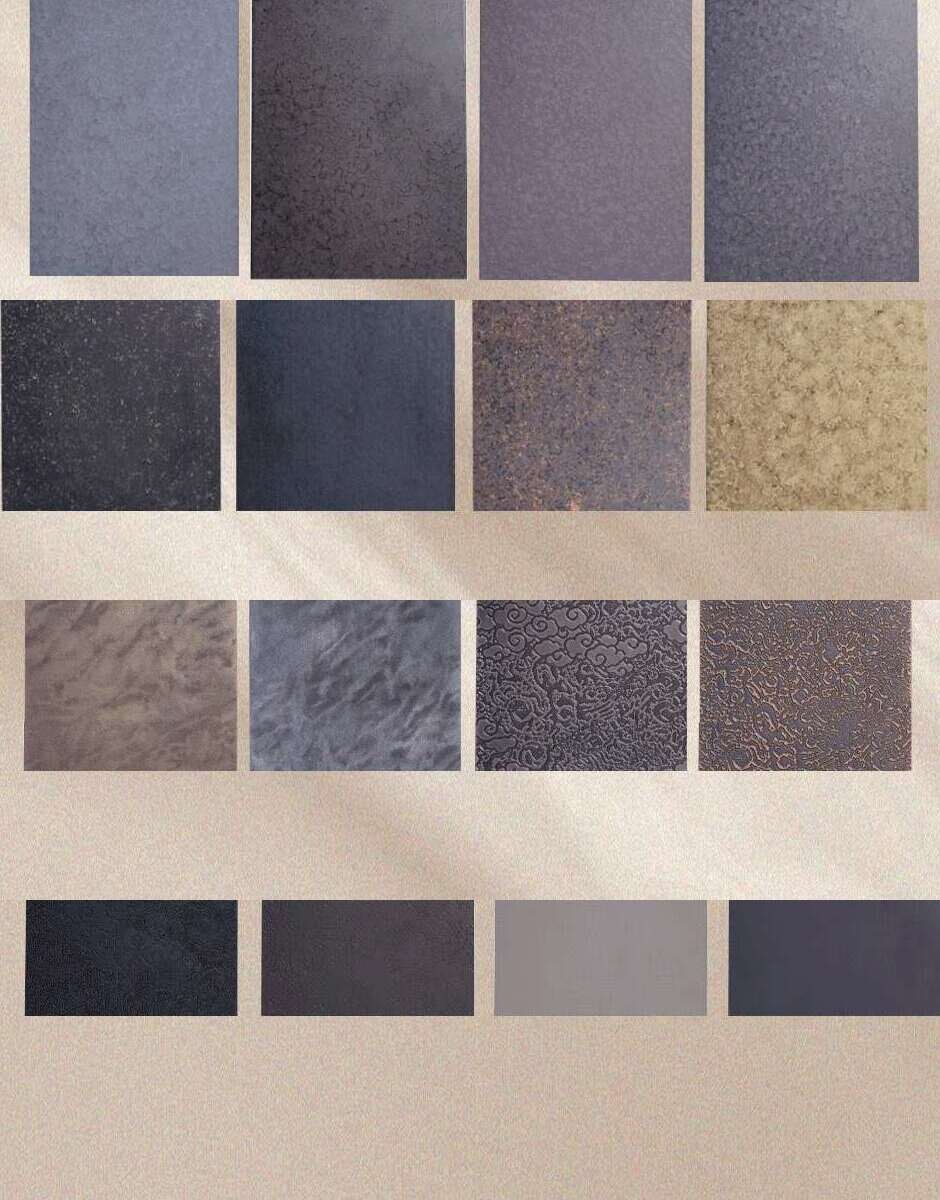
These images establish a design direction only. Colour, gloss, relief, substrate and protective system should be confirmed on a signed physical sample. Exterior exposure, corrosion environment, cleaning method and expected maintenance must also be considered before a finish is approved.
A three-stage control route
Incoming parts
Selected locks, handles and other critical hardware are checked before release to assembly. The inspection plan should identify the drawing or specification, supplier, finish, critical dimensions and functional checkpoints.
In-process inspection
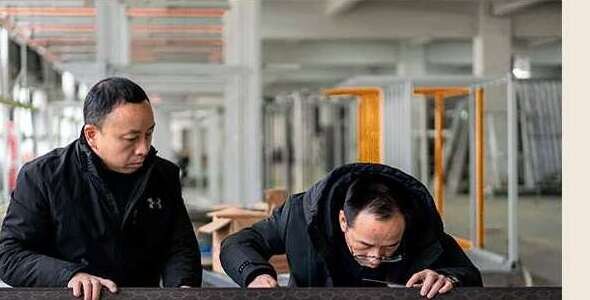
Cross-checks during fabrication help identify dimensional, alignment, preparation and finish problems before they become hidden by later operations. Hold points should match the risks of the actual door construction rather than rely on a generic checklist.
Final release
The completed entrance is reviewed against the approved order and drawings. Typical checks include overall dimensions, squareness and flatness, finish appearance, hardware security, handing, opening and closing, lock operation, seal continuity and completeness of packing.
What an international buyer can request
- Approved drawings, finish sample and hardware schedule.
- Inspection and test plan with defined hold points.
- In-process and final inspection records for the order.
- Photographs of critical details before packing.
- Packing list, labels and traceability references.
- A clear non-conformance and corrective-action route.
The objective is not an abstract “zero defect” slogan. It is a visible process that catches deviations early and gives the buyer a reviewable release record.
This guide is adapted from a quality article first published by EPIN TOMCIM's official WeChat account on 23 May 2026. Finish availability and inspection scope depend on the selected configuration, order and agreed quality plan.